Case Introduction:
A leading bulk cargo port on India's eastern coast handles coal, iron ore fines and slag through a network of underground tunnel conveyors. Among these, BCL-1A and BCL-1B operate under severe impact loading, with material falling from heights of up to 5 metres, making effective impact protection essential for reliable operation.
Issue:
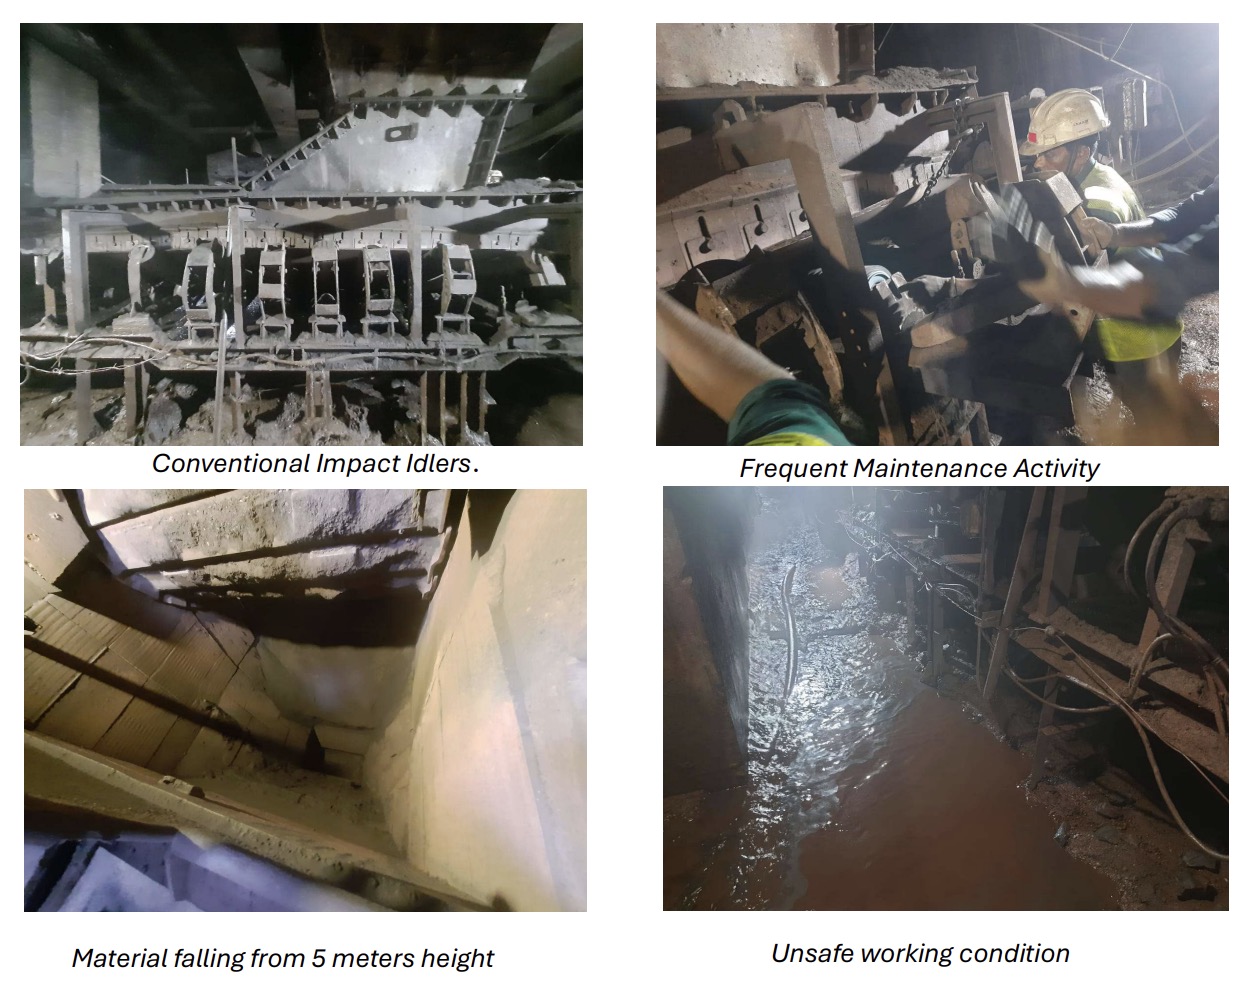
The tunnel conveyors BCL-1A and BCL-1B were experiencing severe operational and maintenance challenges due to conventional impact idlers:
- Frequent impact idler damage due to heavy material loading from 5 meters height
- Impact idlers getting jammed due to material ingress and fines accumulation
- Extremely short idler life of approximately 1 month
- Impact idler maintenance required every week
- Replacement required every 1–2 months
- Severe belt sagging between idlers
- Significant material spillage from skirt zone due to improper belt support
- Manual cleaning required every shift involving 2 personnel for 1 hour
- Frequent shutdowns every 4–5 days for cleaning and maintenance
These issues were further compounded by the underground tunnel environment, making maintenance activities difficult, unsafe, and time-consuming.
Underlying Cause of the Problem:
Tega technical team conducted site inspections and root cause analysis. The primary causes were identified as:
- Heavy impact loading from 5-meter drop height
- Use of conventional and locally fabricated impact idlers with low durability
- Belt sagging between idlers creating gaps in skirt sealing zone
- Ineffective belt support leading to side spillage
- Material ingress causing bearing seizure and idler failure
- Confined underground tunnel environment making replacement and maintenance difficult
These conditions resulted in frequent equipment failure, increased maintenance cost, and operational inefficiency.
Operating Parameters:
| Parameter | Specification |
| Conveyor | BCL-1A / BCL-1B |
| Belt Width | 1400 mm |
| Capacity | 1875 TPH |
| Belt Speed | 2.0 m/s |
| Material | Iron Ore, Coal, Pellets, Slag |
| Material Drop Height | 5 meters |
| Trough | Angle 35° |
| Conveyor Location | Underground Tunnel |
Tega Recommendation:
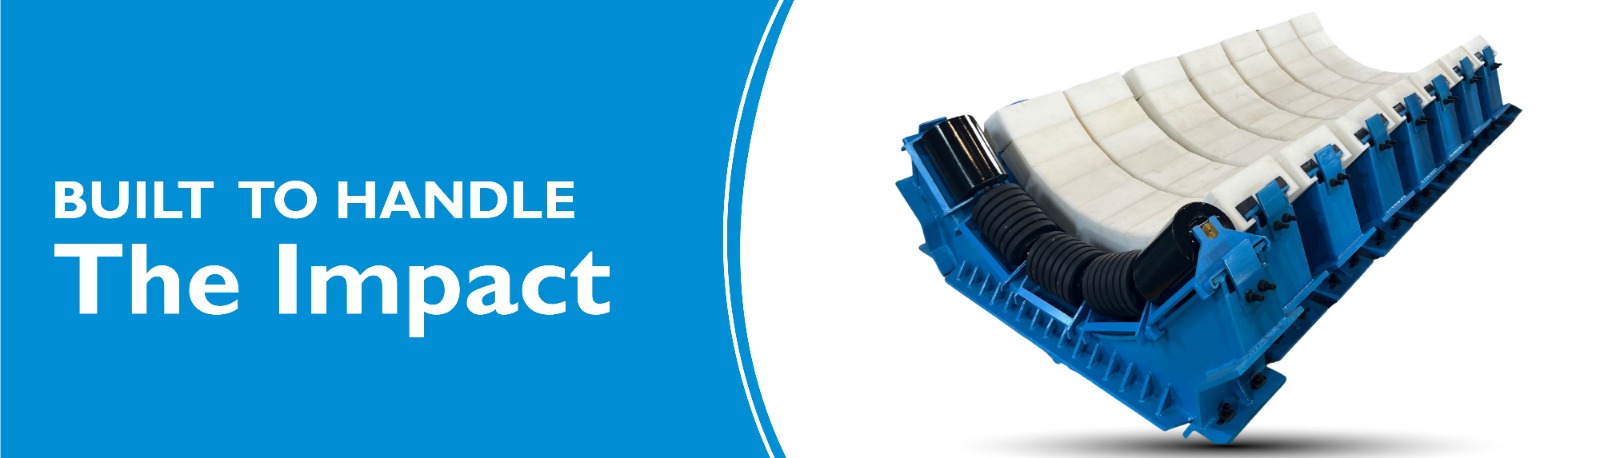
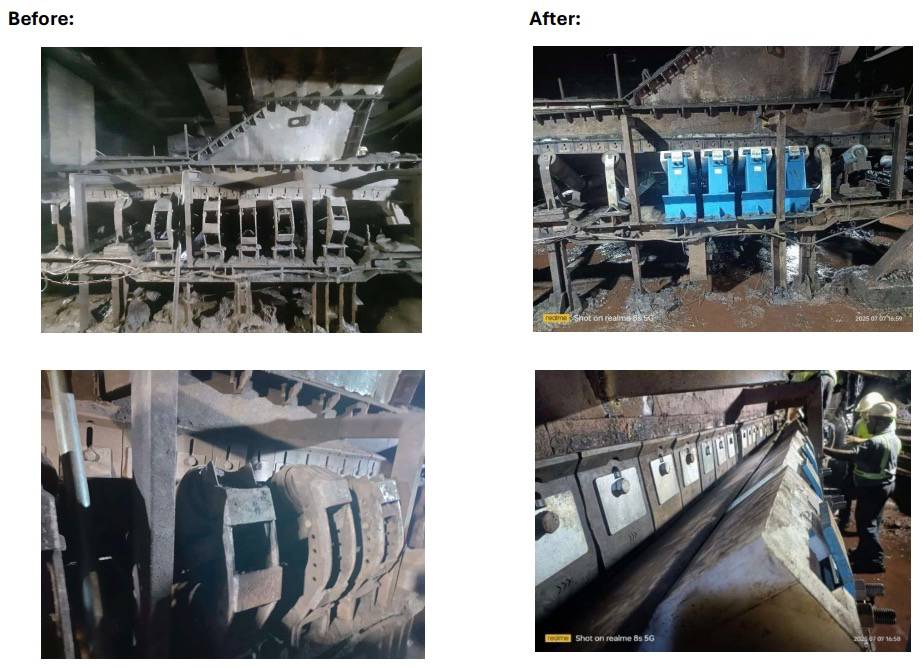
Based on detailed technical evaluation, Tega recommended installation of Tega Jumbo Bed at the loading zones of the tunnel conveyors.
Installed Configuration:
- Conveyor BCL-1A: 4 Modules of Tega Jumbo Bed
- Conveyor BCL-1B: 4 Modules of Tega Jumbo Bed
Tega Jumbo Bed modules were installed directly beneath the loading zone to absorb impact energy and provide continuous belt support throughout the loading area.
| Parameter | Before Jumbo Bed | After Jumbo Bed |
|---|---|---|
| Impact Idler Life | 1 month | Eliminated |
| Maintenance Frequency | Weekly | None |
| Shutdown Frequency | Every 4–5 days | None |
| Belt Sagging | Severe | Eliminated |
| Material Spillage | Heavy | Drastically Reduced |
| Cleaning Frequency | Every shift | Once per week |
| Manpower Requirement | High | Minimal |
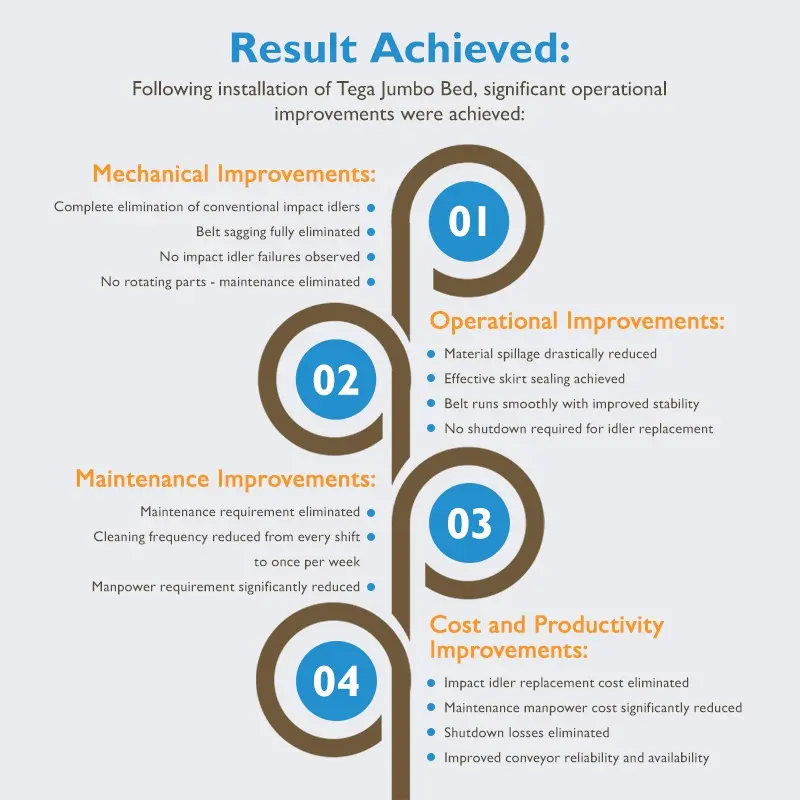
Result Achieved:
Business Impact and Future Potential:
Due to excellent performance of Tega Jumbo Bed at BCL-1A and BCL-1B conveyors, the customer has identified additional conveyors for implementation:
- BCL-2
- BCL-2A
- BCL-9
Customer has identified additional conveyors to implement similar solution.
Conclusion:
The implementation of Tega Jumbo Bed at the port successfully eliminated chronic impact idler failures and drastically reduced material spillage in tunnel conveyors.
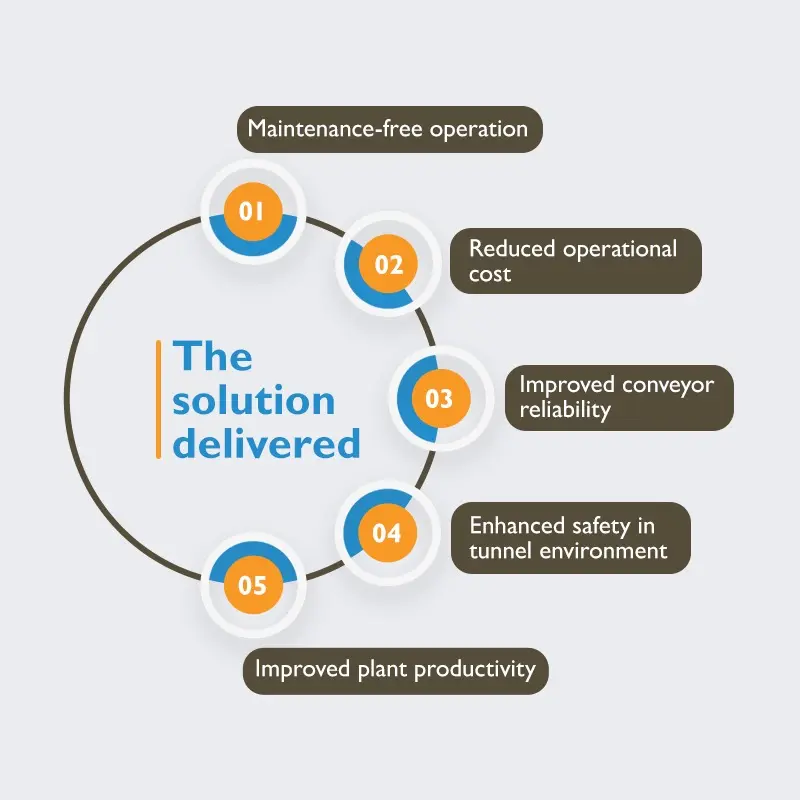
The solution delivered:
 This case demonstrates the effectiveness of Tega Jumbo Bed as a superior and sustainable solution for high impact loading conveyor applications.